Global Market Guide to Specifying Mushroom PLC Control
Immediate Specification Summary

A mushroom PLC control system should be specified as a complete climate-management package rather than as a simple temperature controller. For commercial farms in the Global Market, the control scope normally includes environmental sensors, fans, fresh-air dampers, humidification equipment, cooling and heating devices, compressor protection, recipe-based production stages, touchscreen operation, alarms, remote access, and historical data logging.
The most reliable starting point is to define the crop, room or container size, substrate loading, local climate, electrical supply, cooling method, humidity source, and operating model. Oyster mushrooms, shiitake, button mushrooms, enoki, lion’s mane, and other varieties may require different targets for temperature, relative humidity, carbon dioxide, air movement, lighting, and fresh-air exchange. A controller designed only around one temperature setpoint will not provide the stability required for high-quality fruiting.
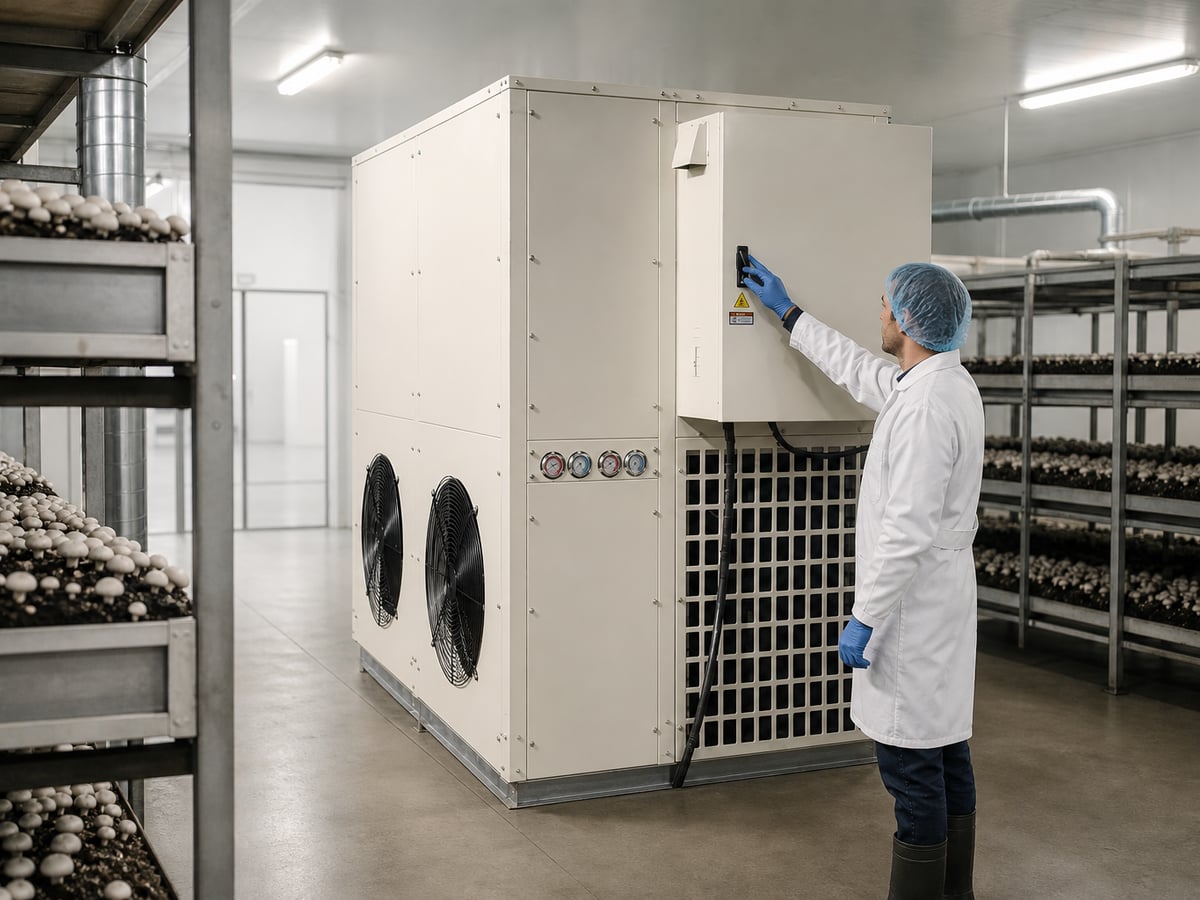
For buyers comparing a stand-alone controller with an integrated cultivation unit, a smart mushroom climate controller can centralize sensor feedback, actuator sequencing, alarms, and production recipes. When a project requires a ready-built growing room with insulated panels, cooling, ventilation, and automation integrated at the factory, a smart mushroom cultivation container can reduce on-site coordination work.
A practical PLC specification should answer these questions before a purchase order is issued:
- What environmental values must be measured in each cultivation zone?
- Which fans, dampers, humidifiers, heaters, refrigeration components, and lights must be controlled?
- Which failures must stop equipment immediately to prevent crop damage or compressor damage?
- How many crop recipes, stages, alarms, languages, and operator access levels are required?
- Does the site need Ethernet, Wi-Fi, cellular communication, cloud data, Modbus, or integration with a farm-management platform?
- Who will commission the system, train operators, provide spare parts, and support remote troubleshooting?
| Specification Area | Minimum Requirement | Recommended Commercial Requirement | Why It Matters |
|---|---|---|---|
| Temperature | One air sensor per room | Multiple calibrated sensors with averaging logic | Reduces false readings caused by cold air discharge or direct humidification. |
| Humidity | One RH sensor | Protected RH sensor plus high/low alarm thresholds | Helps avoid cap cracking, dry substrate, and excessive condensation. |
| CO₂ control | Single CO₂ sensor | NDIR sensor with calibration reminders and fresh-air sequencing | Supports morphology, stem length, yield consistency, and worker safety. |
| Ventilation | Basic fan on/off logic | Variable-speed fans and damper feedback interlocks | Improves air exchange while reducing energy waste. |
| Cooling | Thermostat switching | PLC compressor delays, pressure protection, and staged cooling | Extends refrigeration equipment life and avoids short cycling. |
| Recipes | Manual setpoint adjustment | Multi-stage crop recipes with timed and sensor-based transitions | Standardizes work across shifts, farms, and seasons. |
| Data | Local alarm display | Historical trends, exportable reports, and remote alarm notification | Enables traceability and faster diagnosis of crop incidents. |
The table shows why a professional mushroom PLC system should combine measurement, automation, protection, and reporting. In warm and humid production regions, especially near ports and agricultural logistics centers such as Rotterdam, Dubai, Singapore, Los Angeles, Santos, Melbourne, and Durban, outside-air conditions can change rapidly. The controller must respond predictably without overloading refrigeration or causing sudden humidity loss.
Select Essential Sensor Signals

Sensor selection determines the quality of every control decision. A PLC cannot maintain a stable mushroom climate if the sensors are inaccurate, poorly positioned, unprotected from water spray, or installed where they read discharge air instead of crop-zone conditions. Specify industrial-grade sensors with suitable accuracy, replaceable probes where practical, and clear calibration procedures.
Temperature and relative humidity are fundamental, but they are not enough for most commercial fruiting rooms. Carbon dioxide monitoring is essential where fresh-air demand affects mushroom shape and yield. Differential pressure, air-flow proof, door status, water level, refrigerant safety contacts, and equipment run feedback can also prevent avoidable failures. In larger facilities, separate sensor zones may be needed for the upper and lower rack levels, inlet and return air, and independent growing bays.
| Sensor Input | Typical Signal | Suggested Placement | Control Use |
|---|---|---|---|
| Air temperature | PT100, PT1000, 4–20 mA, or digital | Crop zone, shielded from direct airflow | Cooling, heating, anti-freeze, and recipe control. |
| Relative humidity | 0–10 V, 4–20 mA, or digital | Crop zone with splash protection | Humidification, dehumidification, and condensation prevention. |
| Carbon dioxide | NDIR 0–10 V, 4–20 mA, or Modbus | Representative crop height away from fresh-air inlet | Fresh-air fan and damper demand control. |
| Door switch | Digital dry contact | Personnel and loading doors | Suspends alarms temporarily and records access events. |
| Water tank level | Float switch or analog level sensor | Humidifier tank or supply reservoir | Prevents dry-running pumps and low-water alarms. |
| Airflow proof | Differential pressure switch or current sensor | Supply fan duct or fan panel | Confirms ventilation before enabling cooling or humidification. |
| Coil temperature | NTC, PT100, or digital probe | Evaporator coil or drain pan | Defrost management and coil freeze protection. |
| Outdoor temperature | Weatherproof temperature sensor | Shaded external location | Energy optimization, free cooling, and weather alarms. |
The table provides a baseline input list. For compact mushroom cabins, a single accurate sensor set may be sufficient if air circulation is uniform. For multi-room farms, independent sensors should be assigned to each climate zone. A large room with only one centrally mounted sensor can hide high CO₂ at the back racks, dry air near supply outlets, or elevated temperature near the ceiling.
Specify sensor accuracy in the purchase documentation. For example, temperature accuracy of approximately ±0.3°C to ±0.5°C and humidity accuracy of approximately ±2% to ±3% RH is often appropriate for commercial cultivation. CO₂ sensor range must suit the crop program; many fruiting applications need measurement in the low-thousands ppm range, while incubation or special production steps may require a higher range.
Sensor placement should be agreed during engineering. Do not place humidity sensors immediately beside ultrasonic mist outlets, chilled coils, or doors. Do not mount CO₂ sensors directly in the path of fresh air. Operators should be able to access sensors safely for cleaning and verification. The HMI should also flag impossible or out-of-range values, such as a disconnected 4–20 mA loop or a sensor reading far beyond a realistic operating limit.
List Fans, Dampers, and Compressor Outputs

After defining inputs, identify every controlled output. Each output should have a tag name, electrical rating, control mode, start-stop condition, manual override rule, feedback requirement, and fail-safe state. This prevents common commissioning problems where a fan, valve, damper, or compressor is physically installed but not included in the PLC sequence.
Typical mushroom climate outputs include circulation fans, exhaust fans, fresh-air fans, motorized dampers, cooling compressor contactors, condenser fans, evaporator fans, electric heaters, hot-water valves, humidifier pumps, ultrasonic mist modules, solenoid valves, drain heaters, lighting circuits, and alarm beacons. Variable-frequency drives are increasingly specified for supply and exhaust fans because gradual speed control improves stability and can reduce energy use.
| Output Device | Typical Control Method | Required Feedback or Interlock | Operational Purpose |
|---|---|---|---|
| Circulation fan | On/off or VFD speed command | Motor overload and run-status feedback | Maintains uniform air distribution through racks. |
| Fresh-air fan | On/off, staged, or VFD control | Damper open proof and airflow confirmation | Reduces CO₂ and refreshes room air. |
| Exhaust fan | On/off or proportional speed | Run status and pressure balance logic | Removes stale air and supports controlled ventilation. |
| Fresh-air damper | Open/close or modulating 0–10 V | End switch or position feedback | Prevents uncontrolled outdoor-air entry. |
| Compressor | Contactor or staged refrigeration command | High/low pressure, overload, anti-short-cycle timer | Provides cooling while protecting refrigeration equipment. |
| Humidifier pump | On/off, pulse, or proportional command | Water level, flow proof, and leakage protection | Raises RH without dry-running the system. |
| Defrost valve or heater | Timed or temperature-based sequence | Coil temperature and maximum duration limit | Maintains coil performance in cold, humid operation. |
| Lighting circuit | Scheduled relay output | Manual override and electrical protection | Supports crop-specific light routines and safe access. |
This output schedule should be expanded for the actual project. Include voltage, phase, frequency, full-load current, starter type, VFD details, and whether the output is supplied by the controller manufacturer or connected by the installer. Global projects may use 380–415 V, 50 Hz or 460–480 V, 60 Hz supplies, so the electrical design must match the destination country before manufacturing begins.
For farms near coastal locations or humid tropical markets, specify corrosion-resistant enclosures, protected cable glands, suitable IP ratings, and cabinet ventilation or cooling where ambient electrical-room temperatures are high. If the system is shipped through Qingdao, Shanghai, Ningbo, Hamburg, Jebel Ali, or other major trade hubs, export packing should protect electronics, sensors, and HMI components from salt air and moisture during transit.
Define Interlocks and Protection Logic
Interlocks are the rules that prevent unsafe or damaging equipment combinations. Protection logic should be written in plain language before PLC programming begins. Every actuator should have a safe response to sensor failure, overload trip, water shortage, airflow loss, excessive pressure, power interruption, or communication failure.
Compressor protection is particularly important. A compressor should not restart immediately after a power interruption or a normal cooling stop. The PLC should apply minimum off-time, minimum run-time, high-pressure trip handling, low-pressure protection where applicable, overload monitoring, and alarm acknowledgment rules. When a refrigeration fault occurs, the controller should preserve the alarm history and present operators with a clear corrective action.
| Protection Condition | PLC Response | Reset Method | Reason for Inclusion |
|---|---|---|---|
| High compressor pressure | Stop compressor and generate critical alarm | Manual reset after fault investigation | Prevents damage from blocked condenser airflow or refrigerant faults. |
| Low water level | Disable humidifier pump and misting modules | Automatic after safe water level returns | Protects pumps and avoids dry operation. |
| Fan overload trip | Stop related cooling or humidification sequence | Manual reset after motor check | Prevents operating equipment without essential airflow. |
| Damper fails to open | Limit fresh-air fan start or issue airflow alarm | Automatic or manual according to criticality | Avoids fan strain and ineffective CO₂ control. |
| Coil freeze risk | Stop cooling, initiate defrost, or reduce fan speed | Automatic when temperature returns to limit | Preserves heat-transfer performance and protects the coil. |
| Sensor signal failure | Use safe fallback mode and issue alarm | Automatic after valid signal is restored | Prevents uncontrolled operation based on false data. |
| High room temperature | Activate emergency cooling strategy and escalation alarm | Automatic after recovery, alarm acknowledgment required | Protects the crop during heat waves or equipment failure. |
The table demonstrates that protection logic is not merely an alarm list. It defines what the system does, who can reset it, and whether production may continue safely. Critical faults should have different alarm priorities from advisory notices. For example, a high-temperature crop alarm, compressor high-pressure trip, or electrical safety trip may require immediate notification, while a calibration reminder can be scheduled for maintenance staff.
Door-open logic also deserves attention. During harvesting and loading, the door may remain open long enough for temperature, humidity, and CO₂ to deviate. The controller can delay selected alarms, temporarily adjust ventilation behavior, and record the duration. However, door logic should not disable essential safety protections. Clearly define whether the system returns to automatic control immediately after door closure or uses a recovery period.
Set Recipe Stages and Transition Rules
Recipe control converts crop knowledge into repeatable automation. Instead of relying on operators to change setpoints several times each day, the PLC stores defined production stages and changes targets automatically. A recipe can include temperature, humidity, CO₂, fan speed, fresh-air percentage, lighting schedule, humidification limits, defrost priorities, alarm thresholds, and stage duration.
Recipes should not be copied blindly between regions. A mushroom farm in a cool northern climate may use a different fresh-air strategy from a farm in a hot and humid climate near Kuala Lumpur, Lagos, Mumbai, Cartagena, or Bangkok. External climate, insulation level, refrigeration capacity, substrate strain, and local water quality all affect the most practical recipe.
| Recipe Stage | Primary Controls | Example Transition Rule | Operator Check |
|---|---|---|---|
| Room preparation | Ventilation, sanitation timer, lighting | Advance after cleaning confirmation and stable baseline conditions | Verify empty-room cleaning and sensor status. |
| Loading | Moderate ventilation, door mode, lighting | Advance when substrate loading is completed | Confirm batch number and rack allocation. |
| Incubation | Temperature stability, limited ventilation, humidity control | Advance after elapsed days or operator authorization | Inspect substrate colonization and contamination. |
| Pinning induction | Temperature change, CO₂ reduction, humidity management | Advance after specified induction duration | Confirm pin formation and crop response. |
| Fruiting | CO₂ control, fresh air, RH, cooling, air circulation | Advance based on harvest cycle or operator selection | Monitor cap quality, stem length, and surface moisture. |
| Harvest recovery | Humidity recovery, reduced disturbance, ventilation balance | Advance after recovery timer or next flush condition | Record harvested weight and crop observations. |
| End-of-cycle cleaning | Ventilation, drying, maintenance reminders | Advance after batch closeout approval | Record yield, issues, and sanitation completion. |
The recipe table is a framework rather than a universal setpoint guide. Setpoints must be validated with the chosen mushroom variety and substrate supplier. The best PLC systems permit authorized supervisors to edit recipes, lock critical limits, duplicate proven programs, and export recipe files for use at additional sites.
Transition rules should combine time-based and condition-based decisions. A stage can end after a number of hours, after an operator inspection, after a measured temperature recovery, or after a production manager confirms crop development. This flexibility is valuable because biological production does not always follow a fixed calendar. The HMI should show the current stage, elapsed time, remaining time, active targets, next transition condition, and any manual changes made by the operator.
Design Touchscreen Pages for Operators
A touchscreen should be designed for daily farm work, not just for electrical technicians. Operators need large, understandable values, a clear indication of automatic or manual mode, easy navigation, alarm visibility, and access to current recipe information. Supervisors need deeper pages for setpoint adjustment, historical trends, calibration reminders, user permissions, and maintenance records.
Recommended HMI pages include an overview dashboard, room schematic, live climate values, equipment status, recipe stages, manual control, alarm history, trends, settings, user management, maintenance, and communication status. Use clear color conventions: green for running normally, gray for stopped, amber for warning, red for fault, and blue or another distinct color for manual operation. Colors should never be the only source of information; text labels remain important for operators with different visual needs.
The overview page should display temperature, RH, CO₂, current stage, time remaining, fan status, cooling status, humidifier status, active alarms, and communication state. A room schematic can show dampers, fans, refrigeration, water level, and sensors in a visual layout. This reduces the time needed to identify whether a problem is related to air movement, water supply, refrigeration, or a sensor.
Manual pages must require login permission and should display warnings whenever manual commands override automatic control. Ideally, a manual command has a time limit or returns automatically to recipe control after an approved period. This protects the crop from forgotten overrides after maintenance work.
For global deployment, specify the required HMI language, units, date format, time zone, and user roles. English is widely used in international engineering, but local operators may need additional language support. Temperature units, electrical values, and alarm labels should remain consistent throughout documentation, panel labels, and touchscreen pages.
Confirm Remote Access and Data Options
Remote connectivity can help operators and service teams respond quickly, but it must be designed with cybersecurity and ownership in mind. Decide whether the farm needs remote monitoring only, remote parameter viewing, remote alarm acknowledgment, remote troubleshooting, or controlled remote adjustment. Critical changes should be restricted to authorized users and recorded in the event log.
Available options may include Ethernet, Wi-Fi, 4G or 5G cellular routers, VPN access, Modbus TCP, BACnet gateways, cloud dashboards, local data storage, USB export, email notifications, and mobile alarm messages. Facilities with unreliable internet should retain local PLC control even when cloud access is unavailable. The climate system must continue to run recipes and safety protections autonomously.
Ask for a data list before ordering. Common recorded points include room temperature, RH, CO₂, outdoor temperature, compressor run time, fan speed, damper position, humidifier run time, water level alarms, door-open events, power recovery events, stage changes, manual overrides, and alarm acknowledgments. Trend data allows managers to connect crop outcomes with environmental conditions.
Data retention must match the operating objective. A small farm may require only several months of trend history, while a distributor, contract grower, or multi-site food supplier may need long-term batch records. Export formats should be convenient for analysis, such as CSV-compatible reports or secure dashboard downloads. Clarify whether cloud subscriptions, mobile SIM charges, remote support sessions, or platform licenses are included.
Remote service is especially useful for equipment crossing international borders. A supplier can review alarms and PLC values without waiting for travel arrangements, which can shorten downtime for farms in Africa, Europe, North America, South America, the Middle East, Southeast Asia, and Oceania. However, the customer should control access approval, passwords, user roles, and network connection policies.
Test Automatic and Manual Control Modes
Factory acceptance testing and site commissioning should verify every input, output, alarm, interlock, recipe, and screen. Do not accept a PLC mushroom control system based only on a powered touchscreen demonstration. Functional testing should confirm that field devices respond correctly and that safety logic operates as specified under realistic fault conditions.
Automatic mode testing begins with sensor verification. Compare displayed values with calibrated instruments, check scaling, simulate sensor disconnection where safe, and confirm the correct alarm response. Next, verify each output: circulation fans, fresh-air fans, dampers, humidification devices, cooling stages, heating devices, defrost functions, lighting, and alarm indicators.
Manual mode testing should be done by authorized personnel. Confirm that the operator can start and stop permitted equipment, that unsafe commands are blocked, that manual overrides are prominently shown, and that automatic control resumes correctly. For example, it should not be possible to force a compressor to run when a high-pressure protection input is active, or to run a humidifier pump when low-water protection is triggered.
Commissioning should also test power restoration. After simulated power loss, verify the start sequence, compressor delay, alarm event record, HMI recovery, recipe continuity, and communication reconnection. For containerized projects, test at factory load conditions before shipment whenever possible, then repeat critical checks after installation at the final site.
A documented test checklist is valuable for buyers, contractors, and insurers. It should include equipment tags, test date, responsible person, expected behavior, actual result, corrective action, and final approval. This record creates a stronger handover package and helps maintenance teams understand the original system design.
About Lanhu
Shandong Lanhu Air Conditioning Equipment Co., Ltd. supports mushroom cultivation projects with integrated climate-control engineering for customers across the Global Market. The company is based in Dezhou, Shandong, China, a manufacturing region with established transport connections to Qingdao Port and other international export routes. Its solutions are used by agricultural contractors, equipment distributors, engineering companies, and commercial mushroom producers seeking controlled cultivation environments.
Technological capabilities: Lanhu applies more than 12 years of thermodynamic research and development experience to agricultural climate control, industrial HVAC, modular cultivation environments, smart mushroom controllers, hydroponic plant containers, and air source heat pump systems. Its engineering approach combines refrigeration behavior, air distribution, humidity management, sensor feedback, PLC logic, and recipe-based automation. The company holds multiple registered patents and maintains management and safety certifications including ISO 9001, ISO 14001, ISO 45001, and ISO 12100.
Manufacturing capabilities: Lanhu operates a modern production facility exceeding 30,000 square meters. Internal capabilities include product design, engineering development, sheet metal fabrication, CNC bending, insulated panel production, electrical assembly, system integration, equipment testing, and quality inspection. Functional inspection, electrical verification, performance testing, and operational evaluation are completed before shipment. This integrated process helps align the control cabinet, HVAC equipment, insulation structure, wiring, sensors, and programmed sequence.
Service capabilities: Lanhu provides factory-direct supply, OEM and ODM customization, engineering assistance, international logistics coordination, spare-parts support, installation guidance, and after-sales service. Buyers needing a project-specific enclosure layout, controller branding, special electrical standards, additional sensor inputs, or customized recipe functions can review the company’s OEM and ODM customization services during the planning stage.
For practical examples of integrated controlled-environment projects, buyers can review mushroom cultivation project cases. Case information can help stakeholders compare container layouts, climate-management approaches, production requirements, and installation concepts before selecting their own configuration.
By 2026, mushroom climate automation is expected to move further toward energy-aware control, predictive maintenance, connected farm reporting, and lower-water-use humidification strategies. Buyers increasingly request VFD fan control, high-efficiency refrigeration, heat recovery where feasible, solar-compatible electrical planning, refrigerant compliance awareness, and data-supported crop optimization. Sustainability expectations are also rising as food producers seek lower energy intensity, improved insulation, longer equipment life, reduced crop losses, and traceable operating records.
Frequently Asked Questions
What is the most important sensor in a mushroom PLC control system?
There is no single sensor that can replace the others, but temperature, relative humidity, and CO₂ are the core climate inputs for most fruiting rooms. CO₂ measurement is often overlooked, even though it strongly affects fresh-air decisions and mushroom morphology. Larger rooms may require multiple sensors to represent actual crop-zone conditions.
Should fans run continuously in a mushroom growing room?
Many systems operate circulation fans continuously or at low speed to maintain uniform conditions, while fresh-air and exhaust fans operate according to CO₂, humidity, temperature, schedule, or pressure requirements. The correct strategy depends on crop variety, room design, airflow pattern, and energy targets. Variable-speed fan control provides more flexibility than simple on/off operation.
Why does a compressor need PLC protection logic?
Refrigeration compressors can be damaged by rapid restarting, high pressure, low pressure, overload conditions, poor condenser airflow, and power interruptions. PLC logic can enforce restart delays, run-time limits, alarm escalation, and safe shutdown. This improves reliability and reduces the risk of a cooling failure during a sensitive crop stage.
Can one controller manage several mushroom rooms?
Yes, a PLC can manage multiple rooms if it has sufficient inputs, outputs, communication capacity, and HMI design. Each room should normally have independent sensors, recipe settings, alarms, and output sequences. Separate zones prevent one room’s door opening, harvest activity, or crop recipe from disrupting another room.
What should be included in a factory acceptance test?
The test should cover sensor readings, touchscreen pages, all electrical outputs, alarms, interlocks, compressor delays, fan overload response, water-level protection, damper operation, recipe transitions, manual overrides, power-recovery behavior, and data communication where included. A signed checklist should be supplied with the project documentation.
Is remote access necessary for a small mushroom farm?
Remote access is not mandatory, but it can be highly useful when the farm owner is not always on site. At minimum, remote alarm notification can reduce response time during high-temperature events, power interruptions, water shortages, or refrigeration faults. The control system should still operate locally and safely if internet service fails.
How can buyers compare mushroom PLC control suppliers?
Compare suppliers on sensor quality, control logic detail, electrical documentation, refrigeration protection, recipe capability, HMI usability, local electrical compatibility, factory testing, spare-part availability, remote support, and proven manufacturing capacity. Ask for an input/output list, alarm matrix, control narrative, panel drawings, project examples, and clear warranty terms rather than comparing only the initial price.
Share this article
About the Author: Shandong Lanhu Air Conditioning Equipment
Lanhu is a professional climate control equipment manufacturer specializing in smart agricultural systems, commercial HVAC solutions, and customized temperature control technologies. With extensive engineering experience, Lanhu provides reliable solutions for plant factories, controlled environment agriculture, and industrial applications.
Previous Post
Next Post
Need a Custom Climate Control Solution?
From smart agricultural systems to commercial HVAC solutions, Lanhu provides reliable temperature and humidity control solutions tailored to your project needs.
Contact Us