Commercial Mushroom Cultivation Guide for Global Markets
Quick Answer

Commercial mushroom cultivation is a controlled-environment production system in which substrate quality, sanitation, temperature, humidity, fresh-air exchange, carbon dioxide concentration, lighting, harvesting discipline, and cold-chain handling must work together. For Global Market operators, the most dependable route is to standardize one or two species first, document every production batch, and invest in climate control before expanding grow-room capacity.
Whether producing oyster mushrooms, shiitake, lion’s mane, button mushrooms, enoki, or specialty medicinal varieties, profitability depends less on simply adding more bags or shelves and more on maintaining repeatable fruiting conditions. A well-designed farm separates clean and dirty workflows, keeps incubation and fruiting environments independent, uses measured rather than estimated climate settings, and reacts quickly to contamination or equipment alarms.
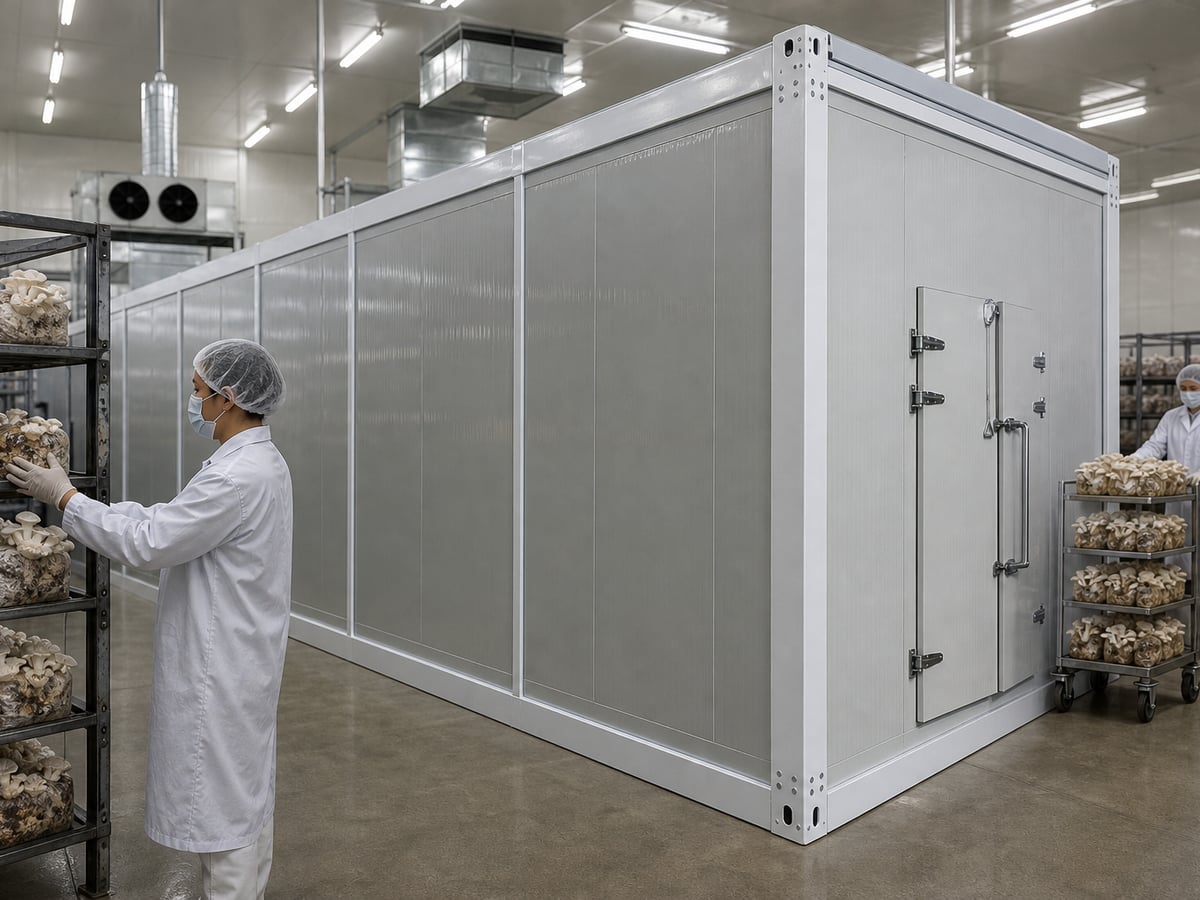
Commercial growers should begin with a defined production target: kilograms harvested per week, target customer channels, available utility capacity, labor availability, and acceptable operating risk. Modular systems can reduce construction time and simplify expansion. For example, a smart mushroom cultivation container can combine insulation, shelving, air treatment, cooling, heating, humidification, ventilation, and monitoring in a compact production unit.
The practical rule is simple: stabilize biology first, then scale capacity. A farm that produces consistent quality from a small number of controlled rooms generally has a stronger foundation than a larger facility with mixed climate zones, unmeasured CO₂ levels, inconsistent substrate, and unclear sanitation practices.
| Commercial Priority | Why It Matters | Basic Operating Target | Management Action |
|---|---|---|---|
| Substrate quality | Determines nutrient availability and contamination risk | Uniform moisture, formulation, and pasteurization or sterilization | Approve suppliers and record each batch |
| Temperature control | Influences colonization speed, pinning, and fruit body quality | Species-specific setpoints with narrow variation | Use calibrated sensors and alarm thresholds |
| Humidity control | Prevents drying, cracking, poor pinning, or excess condensation | Stable relative humidity without surface wetness | Balance humidification with airflow |
| CO₂ management | Affects stem length, cap shape, density, and yield | Measured ventilation response by crop stage | Install dependable CO₂ sensors |
| Sanitation | Limits mold, bacteria, insects, and cross-contamination | Documented cleaning between cycles | Separate personnel and material routes |
| Cold-chain handling | Protects shelf life and customer satisfaction | Rapid cooling after harvest | Plan packing and dispatch windows |
This summary table shows why mushroom production should be treated as a managed biological process rather than a simple indoor farming activity. Every variable affects the others. For example, adding humidity without sufficient airflow can produce wet caps and disease pressure, while adding fresh air without humidity compensation can dry young pins.
What Commercial Operators Should Know About Mushroom Cultivation
The Global Market for fresh and dried mushrooms includes wholesale distributors, supermarkets, hotels, restaurants, food processors, health-food brands, meal-kit suppliers, pharmaceutical ingredient buyers, and direct-to-consumer channels. Demand patterns vary by region. Oyster mushrooms are widely accepted in urban foodservice markets; shiitake has strong retail and Asian cuisine demand; lion’s mane is increasingly positioned in premium culinary and wellness categories; button mushrooms remain a high-volume staple where compost-based production infrastructure is available.
Commercial operators should select species based on customer demand, local logistics, available substrate, climate requirements, shelf life, and crop-cycle complexity. A grower near Rotterdam, Hamburg, Dubai, Singapore, Los Angeles, São Paulo, Johannesburg, Mumbai, or Sydney may have access to different wholesale channels, import competition, labor costs, energy tariffs, and consumer preferences. Export-oriented farms also need to consider packaging standards, phytosanitary requirements where applicable, product traceability, and reliable refrigerated transport.
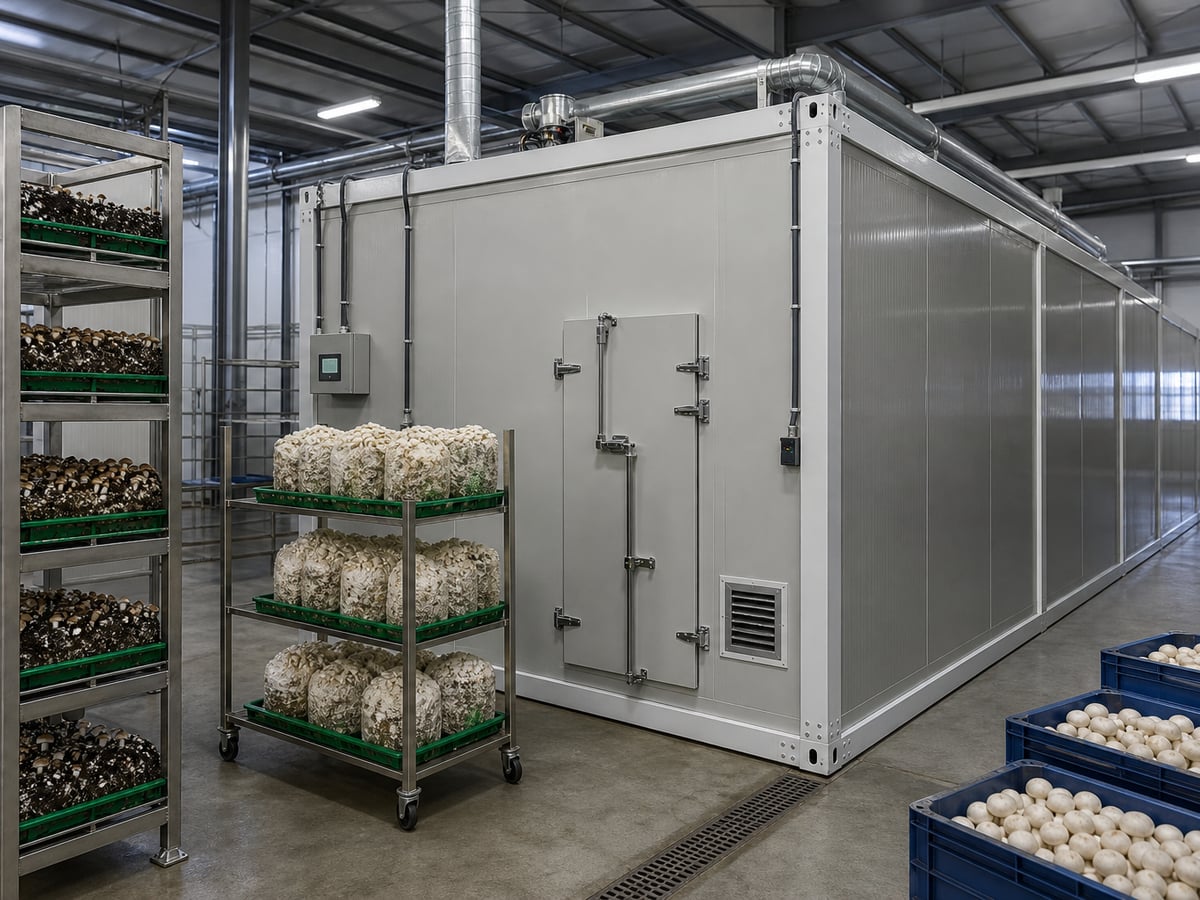
There are several broad commercial production formats. Bag cultivation is common for oyster mushrooms, lion’s mane, shiitake, reishi, and many specialty species. Bottle cultivation is highly automated and frequently used for enoki and shimeji in large industrial operations. Tray, shelf, and bed systems are common in button mushroom facilities. Containerized cultivation can suit pilot projects, remote sites, urban farms, research programs, hospitality groups, and growers seeking modular expansion.
The right business model is often determined before the first crop is inoculated. A farm serving local restaurants may prioritize flavor, freshness, and frequent delivery. A supplier selling through retail chains may require standardized pack weights, barcode labeling, food-safety documentation, and consistent weekly volumes. A dried mushroom or powder producer can tolerate different fresh-grade specifications but must manage dehydration, moisture testing, and storage carefully.
| Production Format | Typical Crop Suitability | Commercial Strength | Main Limitation |
|---|---|---|---|
| Bag cultivation | Oyster, shiitake, lion’s mane, reishi | Flexible, scalable, relatively accessible | High manual handling if not organized |
| Bottle cultivation | Enoki, shimeji, specialty varieties | High automation potential and uniformity | Higher capital and engineering requirements |
| Compost shelf system | Button, cremini, portobello | High-volume production potential | Complex compost and casing management |
| Container farm | Oyster, lion’s mane, shiitake trials | Fast deployment and climate integration | Space must be planned carefully |
| Warehouse grow rooms | Multiple species and larger regional farms | Custom capacity and workflow design | Requires coordinated HVAC and hygiene zoning |
| Hybrid farm | Spawn, incubation, fruiting, packing | Can balance internal production and purchased blocks | More complex supply-chain coordination |
For a new project, purchased colonized substrate blocks can reduce the initial technical burden. This approach allows the operator to focus on fruiting-room management, harvesting, sales, and customer development. Once production is stable, the farm may add substrate preparation, sterilization, inoculation, and incubation. Fully integrated production offers greater control but also introduces additional contamination risk, steam demand, labor requirements, and quality-control responsibilities.
Why It Matters to Yield, Quality, and Operating Risk
Mushroom crops respond quickly to environmental instability. A few hours of excessive heat, low humidity, inadequate ventilation, or water accumulation can reduce quality during sensitive pinning and fruiting stages. In commercial operations, the loss is not only biological. A failed room can disrupt contractual deliveries, overload packing labor on later harvest days, increase waste, and reduce buyer confidence.
Yield is usually evaluated through biological efficiency, kilograms harvested per square meter, kilograms per block, crop-cycle duration, grade-out percentage, and saleable yield. Quality is assessed through cap formation, stem length, color, firmness, cleanliness, uniformity, moisture condition, absence of pests, and shelf life. Operators should distinguish gross harvest from saleable packed product because damaged, overmature, contaminated, or poorly shaped mushrooms may not meet the intended sales channel.
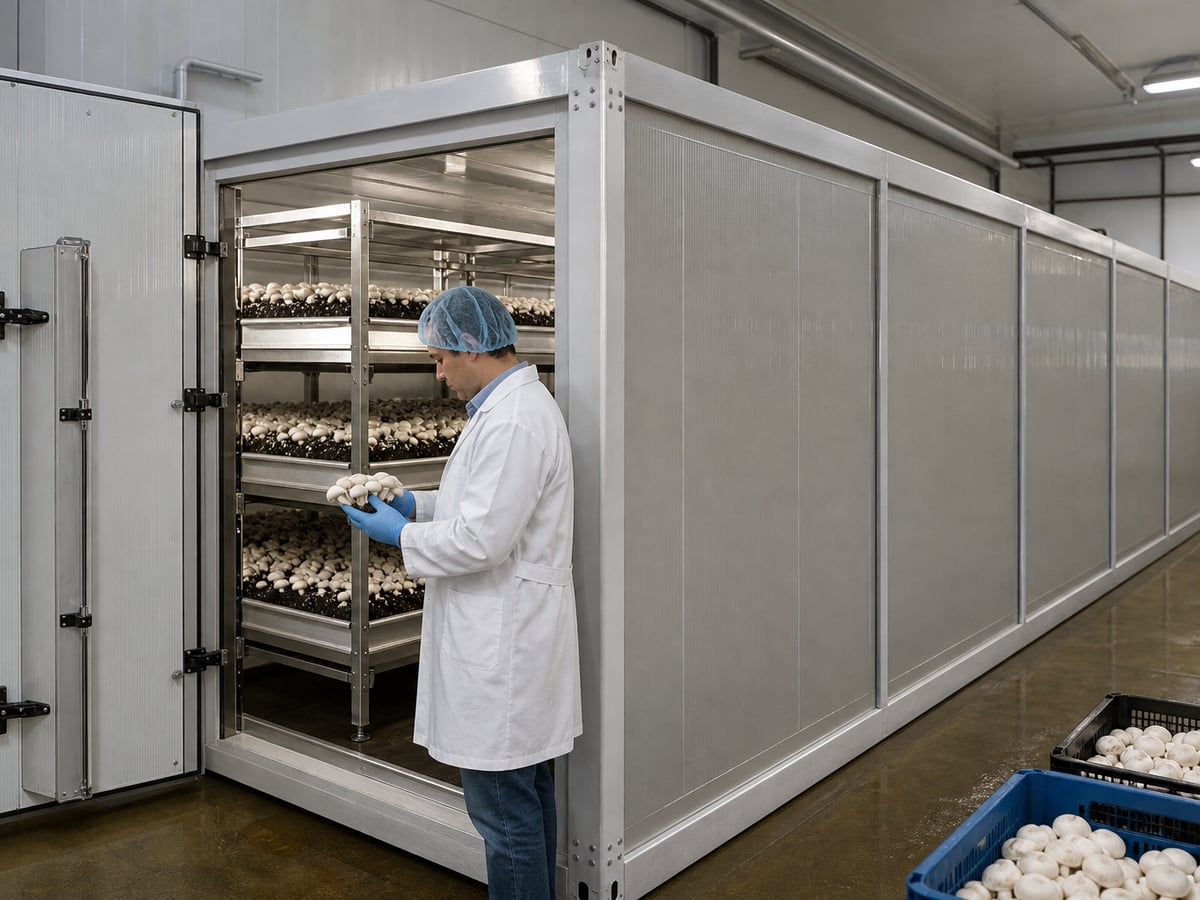
Operating risk is strongly connected to room segregation. Incubation generates heat from mycelial metabolism and often requires different fresh-air levels than fruiting. Fruiting rooms need more controlled ventilation, humidification, and crop observation. Mixing these functions can create unstable conditions and make contamination tracing difficult. Dedicated loading areas, cleaning stations, staff changing points, and waste routes are valuable even in compact facilities.
Climate equipment should be sized for actual heat load, moisture load, external weather, lighting, people, refrigeration losses, and the heat generated by colonizing substrate. Operators in hot-humid ports such as Singapore, Manila, Mombasa, or Santos may need strong dehumidification and cooling strategies. Farms in colder locations such as Toronto, Warsaw, Helsinki, or inland northern China may need reliable heating, insulation, frost protection, and heat-recovery planning.
| Risk Event | Likely Cause | Yield or Quality Impact | Early Warning Indicator |
|---|---|---|---|
| Long stems and small caps | High CO₂ or inadequate air distribution | Lower visual grade and market value | Stretching within early flush development |
| Dry, cracked caps | Low humidity or excessive direct airflow | Weight loss and poor shelf appearance | Pin drying and edge cracking |
| Wet caps and bacterial pressure | Condensation or over-humidification | Reduced shelf life and higher rejection | Water droplets on caps or walls |
| Slow colonization | Incorrect incubation temperature or weak spawn | Longer cycle and contamination exposure | Uneven mycelial coverage |
| Green mold outbreaks | Insufficient sanitation or contaminated substrate | Crop loss and cross-room spread | Localized discoloration and odor changes |
| Harvest inconsistency | Poor scheduling or variable block age | Labor bottlenecks and missed sales orders | Uneven pin sets across shelves |
The table highlights why growers need objective measurements. Visual observation remains essential, but it should be supported by logged room temperature, relative humidity, CO₂, equipment runtime, water use, and batch records. Data allows managers to identify whether a recurring problem is related to one substrate supplier, one room, one shift, one climate setting, or one stage of the crop cycle.
Key Parameters, Measurements, and Design Assumptions
Commercial design begins with crop biology, not equipment catalogs. Temperature, humidity, CO₂, light, airflow, substrate moisture, and sanitation requirements differ by species and strain. Operators should obtain crop instructions from their spawn supplier and validate those targets through controlled trials before committing to large-scale expansion.
For many oyster mushroom varieties, fruiting commonly occurs in relatively cool, humid, well-ventilated conditions, while incubation may require warmer conditions. Lion’s mane often requires high humidity and careful fresh-air management to avoid distorted fruit bodies. Shiitake production is affected by block maturation, induction practices, temperature, and flush management. Button mushroom production depends on compost quality, casing moisture, room climate, and disciplined crop steering.
Design assumptions should include the maximum number of substrate blocks or beds in each room, average substrate weight, expected yield, number of flushes, crop duration, harvest pattern, target temperature range, outdoor design conditions, electrical service, water quality, drainage capacity, refrigeration requirements, and planned future expansion. It is a mistake to size a climate system based only on room volume. Crop load, insulation quality, local weather, and ventilation rates are equally important.
| Parameter | What to Measure | Recommended Instrument | Operational Use |
|---|---|---|---|
| Air temperature | Room air at crop level and supply air | Calibrated digital probe | Controls heating and cooling response |
| Relative humidity | Room humidity and stability over time | Industrial RH sensor | Guides humidification and dehumidification |
| Carbon dioxide | CO₂ concentration by room and crop stage | NDIR CO₂ sensor | Controls fresh-air exchange |
| Surface condition | Condensation, dryness, cap moisture | Visual inspection and records | Confirms airflow and fogging balance |
| Substrate temperature | Internal block or compost temperature | Stainless temperature probe | Detects metabolic heat and overheating |
| Water quality | Hardness, solids, pH, microbial condition | Laboratory or field test kit | Protects humidifiers and crop hygiene |
| Energy consumption | Electricity use by room and equipment | Submetering system | Supports cost control and equipment sizing |
Measurements should be reviewed daily by the production manager and summarized weekly. A single displayed room value is not enough when shelving is dense or airflow paths are complex. Sensors should be located where they represent crop conditions, while periodic handheld checks should confirm whether upper racks, lower racks, doorway zones, and distant corners are operating consistently.
Required Equipment, Controls, and Infrastructure
A commercial mushroom facility normally requires insulated rooms or modules, racking or shelving, heating and cooling equipment, humidification, ventilation fans, air distribution ducting, filtered air in appropriate areas, drainage, washable interior surfaces, lighting, electrical distribution, water treatment where needed, and monitoring controls. Depending on the production model, additional equipment may include substrate mixers, bagging machines, sterilizers, boilers, autoclaves, inoculation benches, clean rooms, refrigeration units, packing equipment, and waste-handling systems.
Climate control is the operating core of the fruiting room. A properly selected system must respond to cooling, heating, humidification, ventilation, and dehumidification needs without producing damaging direct drafts or temperature swings. A smart mushroom climate controller can consolidate sensor inputs and automate coordinated responses for temperature, humidity, CO₂, fans, fresh-air dampers, alarms, and scheduled crop stages.
Lanhu’s technological capability is relevant to projects that need integrated agricultural climate management. The company applies more than 12 years of thermodynamic research and development experience to controlled cultivation equipment, including climate controllers, modular mushroom systems, hydroponic containers, and air-source heat pump solutions. For commercial farms, the value is not simply automation; it is the ability to coordinate multiple environmental variables through a practical operating interface.
Infrastructure must also support hygiene. Floors should drain effectively. Walls and ceilings should resist moisture and allow cleaning. Electrical equipment should be suitable for humid environments. Doors should seal while allowing safe movement of carts. Intake and exhaust locations should minimize re-entry of contaminated air. Reliable backup procedures are essential in locations with unstable utility supply.
| Infrastructure Element | Primary Function | Selection Consideration | Failure Prevention Benefit |
|---|---|---|---|
| Insulated panels | Reduce heat gain and loss | Panel thickness, joints, moisture resistance | Improves climate stability and energy efficiency |
| HVAC and heat pump system | Cooling and heating | Local weather, crop heat load, redundancy | Limits temperature excursions |
| Humidification system | Maintains crop moisture environment | Droplet size, water quality, maintenance access | Reduces drying and uneven pinning |
| Fresh-air and exhaust system | Controls CO₂ and air freshness | Airflow pattern, filtration, fan capacity | Prevents poor morphology from stagnant air |
| Racking system | Uses vertical growing space | Load rating, aisle width, cleanability | Supports safe and efficient harvesting | Drainage and washable surfaces | Supports sanitation | Slope, drain capacity, material durability | Reduces standing water and microbial buildup | Monitoring and alarms | Detects deviations early | Remote access, data logging, sensor calibration | Shortens response time during faults |
Manufacturing capability matters when equipment must fit site restrictions, container dimensions, local voltage, room layout, shelving density, or climate load. Shandong Lanhu Air Conditioning Equipment Co., Ltd. operates a modern manufacturing facility in Dezhou, Shandong, with integrated capabilities covering product design, engineering development, sheet-metal fabrication, CNC bending, insulation panel production, electrical assembly, system integration, testing, and quality inspection. This integrated approach can help reduce coordination gaps between structure, climate equipment, and controls.
Recommended Workflow and Operating Procedure
A reliable workflow separates incoming materials, clean production, fruiting, harvesting, packing, waste removal, and cleaning. The exact sequence depends on whether the farm purchases ready-to-fruit blocks or produces its own substrate. In either case, each batch should have a unique identification code showing species, strain, substrate source, inoculation date, incubation date, fruiting-room entry date, harvest dates, and observed issues.
For farms purchasing colonized blocks, the workflow begins with supplier verification and receiving inspection. Check block condition, visible contamination, moisture balance, packaging integrity, and batch age. Move blocks into designated staging or incubation areas, then introduce them to fruiting rooms according to a schedule that smooths weekly harvest volume. Avoid filling an entire room with blocks of mixed ages unless the crop plan specifically supports this approach.
For integrated farms, substrate preparation and inoculation require more stringent hygiene. Raw materials should be stored dry and protected from pests. Pasteurization or sterilization should be validated. Inoculation should occur in a clean, controlled area using trained personnel and sanitized tools. Incubation rooms should be monitored for overheating because mycelial metabolism can raise internal substrate temperatures above room air temperature.
- Confirm customer orders, target harvest dates, and expected weekly volume.
- Inspect spawn or colonized substrate and record lot numbers.
- Clean and verify the assigned incubation or fruiting room before loading.
- Set crop-stage climate recipes and confirm sensor operation.
- Load blocks or trays using a defined shelf map and batch sequence.
- Inspect crops at least once daily for pins, surface moisture, contaminants, and morphology.
- Harvest at the agreed maturity stage, sort immediately, and move product to cooling.
- Clean tools, remove waste, review climate data, and close the batch record.
Harvesting should be timed for market specifications rather than maximum size alone. Restaurant buyers may prefer clustered oyster mushrooms with a particular cap opening. Retail packs may require more uniform individual pieces. Specialty mushroom customers may pay for premium appearance, but they also expect product that is clean, dry enough for packaging, and cooled promptly.
After each crop cycle, remove all residual material, wash room surfaces, clean racks, inspect drains, sanitize as appropriate, and allow time for drying. Equipment filters, humidification nozzles, fan belts, drain traps, and sensor housings should be included in preventive maintenance routines. A facility that is cleaned only after visible contamination appears is already operating behind the risk curve.
Capacity, Energy, Labor, and Cost Considerations
Commercial capacity should be calculated from saleable output, not nominal room size. A rack system may hold a certain number of blocks, but actual weekly sales depend on crop cycle duration, flush pattern, expected yield, cull rate, harvest labor, packing capacity, and order consistency. Expansion should be staged so that sales, labor, and cold storage grow with production.
Energy costs are strongly affected by local climate, insulation, room loading, fresh-air requirements, humidity strategy, equipment efficiency, and operating discipline. In hot locations, cooling and moisture removal can dominate. In cold climates, heating and ventilation heat loss may be significant. In all regions, poor door discipline, air leakage, dirty coils, scaled humidifiers, and weak insulation increase utility costs.
Labor often becomes the limiting factor before room capacity does. Harvesting, trimming, sorting, packing, sanitation, delivery preparation, and recordkeeping require predictable staffing. Farms should identify peak harvest days and avoid crop schedules that create unmanageable labor spikes. Standardized tray sizes, cart routes, rack layouts, labels, and packing procedures reduce time per kilogram.
| Cost Category | Typical Cost Driver | Control Method | Expansion Trigger |
|---|---|---|---|
| Substrate or blocks | Supplier price, freight, loss rate | Benchmark yield by supplier and batch | Stable demand and proven crop performance |
| Energy | Cooling, heating, ventilation, humidification | Submetering, insulation, preventive maintenance | Utility capacity review before adding rooms |
| Labor | Harvest peaks, packing, cleaning | Staggered loading and standard work instructions | When labor utilization remains consistently high |
| Packaging | Pack format, labeling, retail requirements | Match packaging to shelf-life needs | When larger buyers require standardized packs |
| Freight and delivery | Distance, temperature control, order frequency | Route planning and local distribution partnerships | When delivery cost per kilogram declines | Maintenance | Filters, sensors, water systems, fans | Scheduled inspection and spare parts stock | Before equipment utilization becomes critical | Compliance and testing | Food safety, labeling, local permits | Documented procedures and traceability | Before entering regulated retail channels |
The table should be used as a planning framework rather than a fixed budget. Equipment prices, energy tariffs, labor rates, import duties, and construction costs vary substantially between countries. Projects near major trade hubs such as Jebel Ali, Antwerp, Shanghai, Durban, Houston, or Melbourne should also assess freight access, local technical support, spare-part lead times, and the availability of food-grade packaging supplies.
This illustrative chart is not a universal budget. It demonstrates why commercial operators should measure costs by production batch and sales channel. A high-value local restaurant market may justify more labor and packaging, while a wholesale model may require lower unit costs and higher throughput.
Common Mistakes, Failure Modes, and Corrective Actions
The most common commercial mistake is expanding production before repeatable climate control and sanitation are established. Operators may see strong early demand, fill every available shelf, and then discover that labor, cooling, packing, or delivery capacity cannot support harvest peaks. The result is missed harvest windows, reduced quality, and unnecessary waste.
Another common failure is controlling rooms by intuition alone. A grower may raise humidity whenever caps appear dry, but the actual issue may be excessive fresh air, warm supply air, poor rack airflow, or an inaccurate sensor. Likewise, increasing ventilation to reduce CO₂ can unintentionally dry the crop if the moisture load is not compensated. Corrective actions should be based on measured conditions and crop observations together.
Contamination events require disciplined response. Isolate affected blocks or trays immediately, photograph and record the issue, inspect neighboring batches, review supplier and room records, and clean the affected zone. Do not move contaminated material through clean areas. Repeated outbreaks should trigger a root-cause review covering substrate, inoculation hygiene, water, ventilation, drainage, room cleaning, worker movement, and waste handling.
Equipment neglect is also expensive. CO₂ sensors drift, filters clog, drain pans accumulate biofilm, humidifier nozzles scale, and fans lose performance. Preventive maintenance is less costly than responding to an alarm during a critical fruiting period. Keep essential spare parts, define escalation contacts, and test alarm notifications before peak production periods.
| Common Mistake | Typical Result | Corrective Action | Preventive Practice |
|---|---|---|---|
| Mixing crop stages in one room | Conflicting climate requirements | Separate batches and create stage zones | Plan dedicated incubation and fruiting capacity |
| Ignoring CO₂ measurement | Poor shape and inconsistent crop quality | Install and calibrate sensors | Review daily CO₂ trends |
| Over-fogging the room | Condensation, disease, wet product | Reduce fogging and improve airflow balance | Use humidity control logic, not manual guessing |
| Poor drain cleaning | Odors, insects, microbial buildup | Clean, flush, and inspect drainage | Include drains in sanitation checklists |
| Scaling without market contracts | Unsold fresh product and price pressure | Build diversified customer channels | Match room loading to confirmed demand | No batch records | Cannot identify causes of poor performance | Introduce lot tracking immediately | Use standardized production logs | Buying equipment only by price | Insufficient capacity or unreliable control | Reassess load calculations and service support | Compare lifecycle cost and technical suitability |
The corrective-action table is most effective when it becomes part of staff training. Supervisors should review recurring deviations during weekly production meetings and assign a clear owner, deadline, and verification method for each corrective action.
Implementation Checklist for a Commercial Project
A commercial mushroom project should move through feasibility, engineering, procurement, commissioning, trial production, and controlled scale-up. Start by confirming the customer and product strategy. Decide whether the farm will serve nearby restaurants, regional distributors, retail chains, processors, exporters, or a mix of channels. Then choose species and production format based on the required quality, volume, and shelf life.
- Define target species, pack formats, weekly sales volume, and customer segments.
- Assess the local market, competitor supply, freight routes, and available cold-chain services.
- Confirm site utilities, drainage, water quality, electrical capacity, and backup power options.
- Prepare room layout drawings with separate clean, fruiting, packing, storage, and waste routes.
- Calculate climate loads using crop density, insulation, outdoor weather, and ventilation requirements.
- Select controls with temperature, humidity, CO₂, alarm, and data-logging functions.
- Develop written sanitation, harvesting, packing, maintenance, and traceability procedures.
- Run pilot batches before committing to full-capacity customer contracts.
- Measure yield, grade-out, energy use, labor hours, and customer complaints by batch.
- Expand only after the first production module achieves consistent performance.
Lanhu’s manufacturing strength supports projects requiring factory-integrated modular cultivation systems. Its production processes include engineering design, metal fabrication, insulation-panel production, electrical assembly, system integration, functional inspection, electrical verification, performance testing, and operational evaluation before shipment. The company holds ISO 9001, ISO 14001, ISO 45001, and ISO 12100 certifications, supporting a structured approach to quality, environmental management, occupational safety, and machine safety.
For buyers who need project-specific configurations, service capability is equally important. Lanhu provides factory-direct supply, OEM and ODM customization, engineering assistance, international logistics support, spare-parts support, installation guidance, and after-sales service for agricultural contractors, distributors, engineering firms, and commercial farms. Operators can review suitable configurations through the company’s commercial cultivation project cases, discuss private-label or tailored systems through its OEM and ODM service, or request project communication through the commercial project contact page.
Looking toward 2026 and beyond, commercial mushroom cultivation will increasingly combine remote monitoring, predictive maintenance, recipe-based climate automation, energy-efficient heat pumps, water-saving humidification, renewable-energy integration, traceable batch records, and lower-waste substrate strategies. Sustainability requirements are also likely to influence buyer decisions, particularly in markets where retailers and foodservice groups request evidence of energy management, packaging reduction, local production, worker safety, and responsible disposal or reuse of spent mushroom substrate.
FAQ
Which mushroom species are best for a new commercial farm?
Oyster mushrooms are often suitable for first-stage commercial projects because they have broad culinary demand, relatively short crop cycles, and compatibility with bag or block production. However, the best choice depends on local buyers, available substrate, climate conditions, and the operator’s sales strategy. Start with species that customers already understand and purchase consistently.
Should a commercial grower make substrate or buy ready-to-fruit blocks?
Buying colonized blocks reduces initial process complexity and can speed up market entry. Producing substrate internally may improve long-term control and margins at scale, but it requires more equipment, sanitation discipline, technical knowledge, and labor. Many successful operators begin with purchased blocks and integrate upstream production later.
Why is CO₂ control important in mushroom fruiting rooms?
CO₂ is a direct indicator of ventilation demand and strongly affects mushroom shape and development. Excess CO₂ can cause long stems, smaller caps, dense clusters, and inconsistent morphology. The correct target varies by species and crop stage, so growers should use calibrated sensors and follow validated crop recipes.
Can a shipping container be used for commercial mushroom cultivation?
Yes. An insulated, properly engineered container can be an effective solution for pilot farms, urban production, remote agricultural sites, hospitality projects, and phased commercial expansion. It must include sufficient cooling, heating, humidification, airflow distribution, drainage, racking, controls, and access for cleaning and harvesting.
What are the main causes of contamination?
Common causes include contaminated substrate, weak spawn, poor pasteurization or sterilization, inadequate cleaning, standing water, dirty tools, unfiltered or poorly managed airflow, pest entry, and improper worker movement between dirty and clean areas. Batch records are essential for identifying repeated sources.
How can mushroom farms reduce energy consumption?
Use high-quality insulation, correctly sized climate equipment, efficient heat pumps where suitable, well-sealed doors, preventive maintenance, submetering, balanced ventilation, and climate recipes that avoid excessive simultaneous heating, cooling, humidification, and exhaust. Energy efficiency should be evaluated alongside crop quality, not as an isolated objective.
What should buyers ask an equipment supplier before ordering?
Ask for climate-load assumptions, equipment capacity, control functions, insulation specifications, electrical requirements, maintenance access, sensor types, spare-part availability, installation support, warranty terms, shipping arrangement, and examples of similar projects. Buyers should also confirm how the system will perform under their local outdoor climate and intended crop density.
Share this article
About the Author: Shandong Lanhu Air Conditioning Equipment
Lanhu is a professional climate control equipment manufacturer specializing in smart agricultural systems, commercial HVAC solutions, and customized temperature control technologies. With extensive engineering experience, Lanhu provides reliable solutions for plant factories, controlled environment agriculture, and industrial applications.
Need a Custom Climate Control Solution?
From smart agricultural systems to commercial HVAC solutions, Lanhu provides reliable temperature and humidity control solutions tailored to your project needs.
Contact Us